Prepare the carton
Form the carton and make and insert its PE liner from roll film.
Packaging lines for powder coatings, built around the AVANTECHNO F-Series.
Combine automatic carton preparation and PE liner insertion with filling, weighing and final carton sealing in one connected packaging process.
AVANTECHNO brings its own filling equipment together with machines from specialist manufacturers and the conveyors and interfaces required for the agreed layout.
Three machine stages — from carton preparation to final sealing.
Form the carton and make and insert its PE liner from roll film.
Fill to the target weight, then verify the carton on independent check scales.
Fold the upper flaps and apply adhesive tape. The carton leaves ready for further handling.
Illustrative process arrangement. Equipment selection, interconnecting conveyors and operator access are defined for each project.
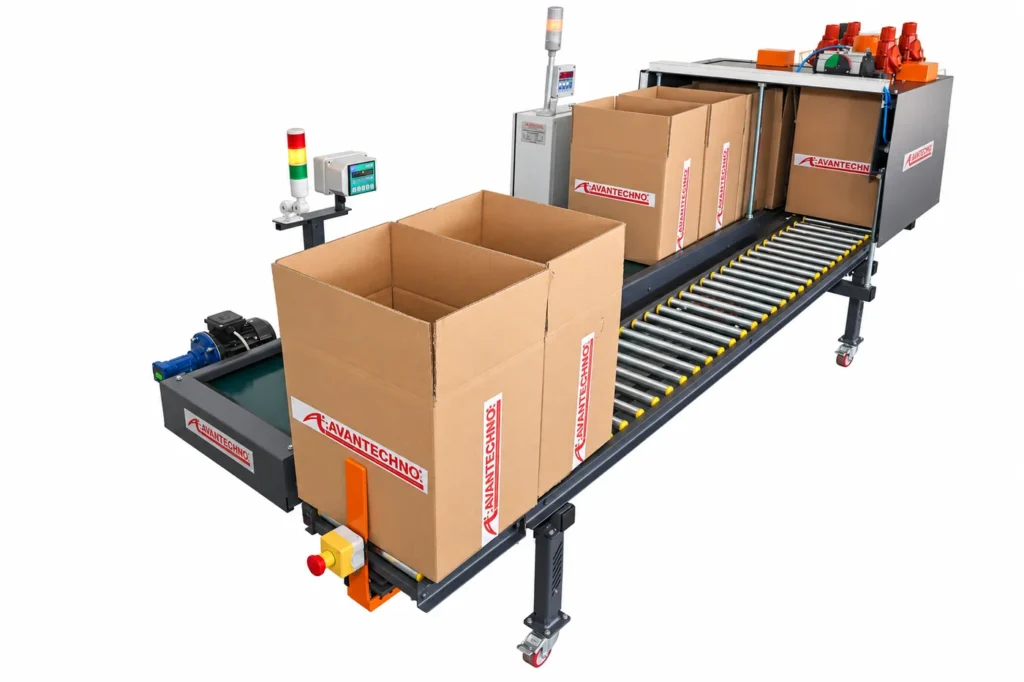
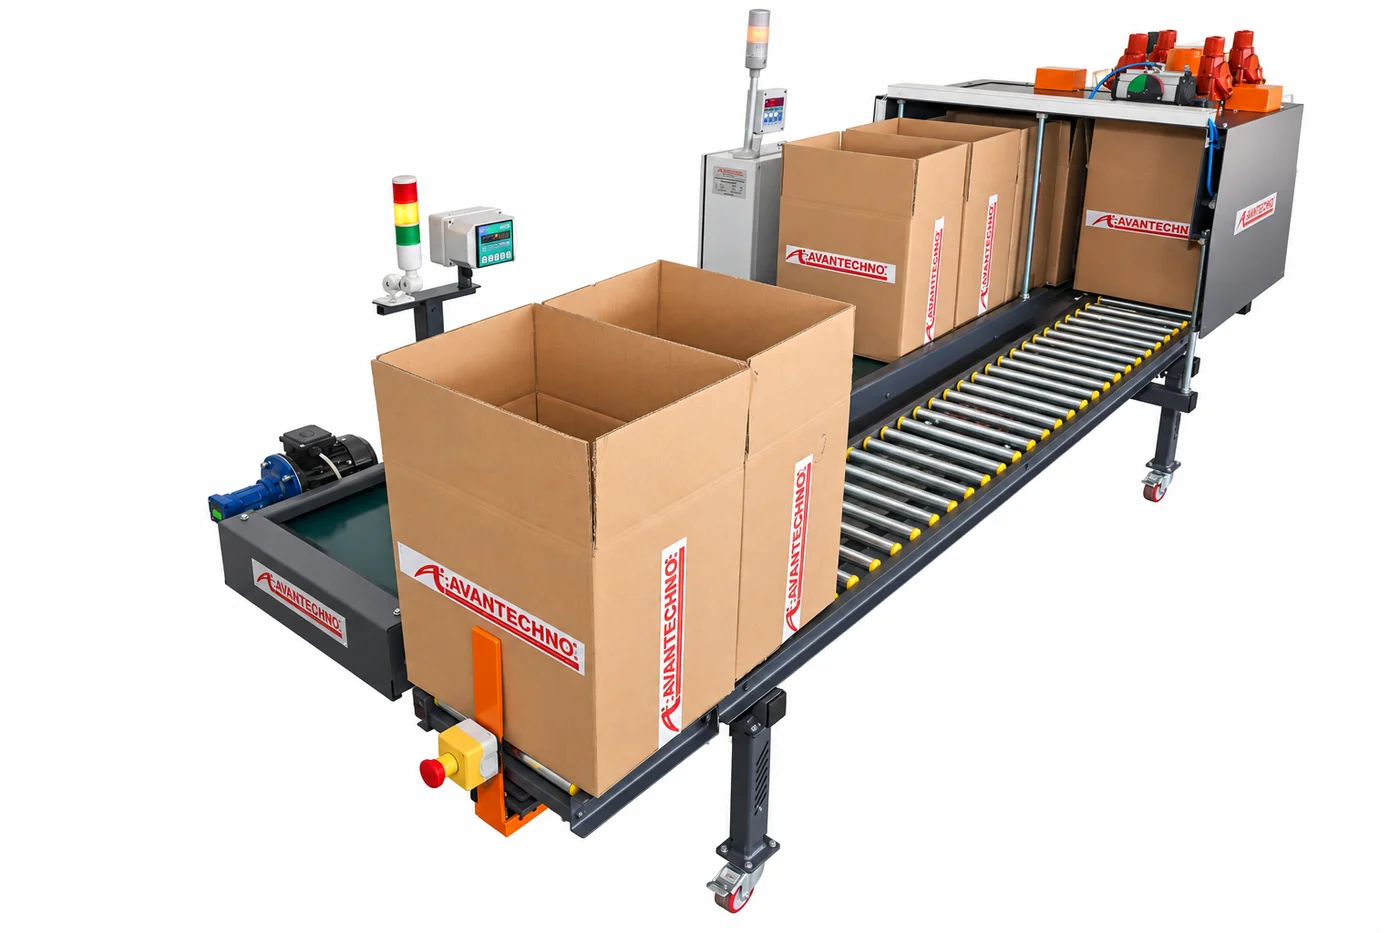
The AVANTECHNO F21 / F31 receives prepared cartons, positions each one beneath the dosing valve and fills it by weight.
The valve closes when the programmed target is reached. The carton is transferred to the roller conveyor, and the next carton enters the filling position.
Independent check scales give the operator a final weight reading and a traffic-light indication of whether the carton is below, within or above the preset tolerance. Any required correction is made before the PE liner is closed.
The case erector and PE liner inserter turn flat corrugated blanks and roll-stock film into cartons ready for filling.
In the reference configuration, the MTW-TK50 forms the carton and makes each liner by sealing and cutting polyethylene film from a roll. The finished liner is then inserted into the formed carton.
Carton forming and liner insertion take place within one automated cycle. Supplying film as roll stock removes the separate feed of pre-made PE bags.
After filling, the operator verifies the final weight, makes any necessary correction and closes the PE liner manually.
The connecting conveyor provides a place for this operation before the carton enters the automatic sealer. Working height, access and space for handling the carton are part of the line layout.
With the inner liner closed, the filled carton enters the automatic case sealer. The machine folds the upper flaps and seals the carton with adhesive tape.
The carton format is adjusted before production. Once set, the machine processes cartons of the same dimensions automatically.
The reference SM11 configuration uses side drive belts and interchangeable taping units for 50 or 75 mm tape. Top-only or top-and-bottom sealing is selected to suit the packaging process.
Connecting conveyor sections are defined around machine spacing, transfer heights and the operator’s liner-closing station.
Machine positions, carton flow and access for loading, adjustment and maintenance are considered together within the available production space.
Electrical supply, compressed air, the powder feed connection and aspiration interfaces are confirmed for the selected equipment and site.
A representative combination for a 400 × 300 × 400 mm carton with a PE liner. Equipment and settings are confirmed for the intended package and production arrangement.
| Stage | Reference equipment | Function | Key reference parameters |
|---|---|---|---|
| Carton preparation | MTW-TK50 | Automatic case erection and PE liner insertion | Reference carton: 300 × 400 × 400 mm PE film: 30–100 μm |
| Filling & weighing | AVANTECHNO F21 / F31 | Filling by weight and independent check-weighing | Carton: 400 × 300 × 400 mm Maximum filled carton weight: 50 kg |
| Carton sealing | SM11 | Automatic upper-flap closing and tape sealing | Maximum carton weight: 32 kg Tape width: 50 / 75 mm |
The maximum filled carton weight for the complete line is determined by the selected downstream equipment. In this reference combination, the sealer is rated for cartons up to 32 kg.
The project combines the preparation machine, AVANTECHNO filling and weighing equipment, the carton sealer and the agreed conveyor sections and line interfaces.
The packaging scope runs from flat carton preparation to the sealed carton leaving the line for further handling or palletizing.
On-site installation, commissioning and operator training can be included in the project.
The service scope is defined around the final configuration and site conditions, with the required utilities and connections agreed before commissioning.
AVANTECHNO LTD («АВАНТЕХНО» ООД)
VAT no: BG207775020
1 Keramika str., Sliven 8800, Bulgaria